


Pharmaceutical products are among the most sensitive and highly regulated goods transported globally. From temperature-sensitive formulations to moisture-reactive intermediates, these products demand uncompromising protection throughout the supply chain. Without the right packaging solution, fluctuations in climate, exposure to UV light, or oxygen ingress can degrade their efficacy—or worse, compromise patient safety.
We specialise in high-performance aluminium barrier foil packaging solutions engineered to meet the strict standards of the pharmaceutical industry. Our materials provide total climatic protection, ensuring that your products remain stable, safe, and compliant from manufacturing to end-use.
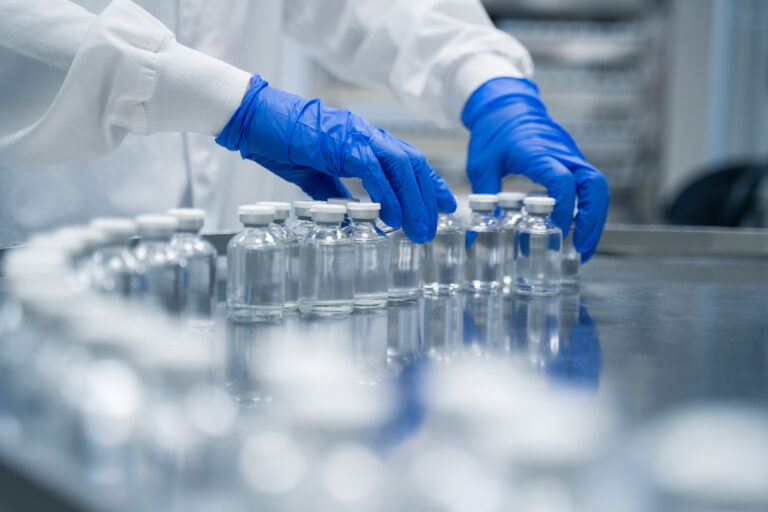
The Climatic Challenge in Pharma Logistics
Pharmaceuticals are vulnerable to a wide range of environmental stressors:
- Moisture ingress that degrades active ingredients
- Oxygen exposure that accelerates chemical breakdown
- Temperature fluctuations that affect shelf life
- UV light and odour transfer that compromise product purity
These factors don’t just threaten quality—they can result in failed compliance, costly recalls, and harm to consumers. That’s why choosing the right packaging partner is critical.
Aluminium Barrier Foil: The Gold Standard in Pharmaceutical Protection
With nearly 35 years of experience, we operate under the globally recognised ISO 9001 Quality Management System. This certification reflects our commitment to consistently delivering quality packaging materials that meet both customer expectations and regulatory requirements.
By adhering to these standards, we provide our clients with peace of mind, they know they’re working with a packaging partner that prioritises reliability, traceability, and continuous improvement.

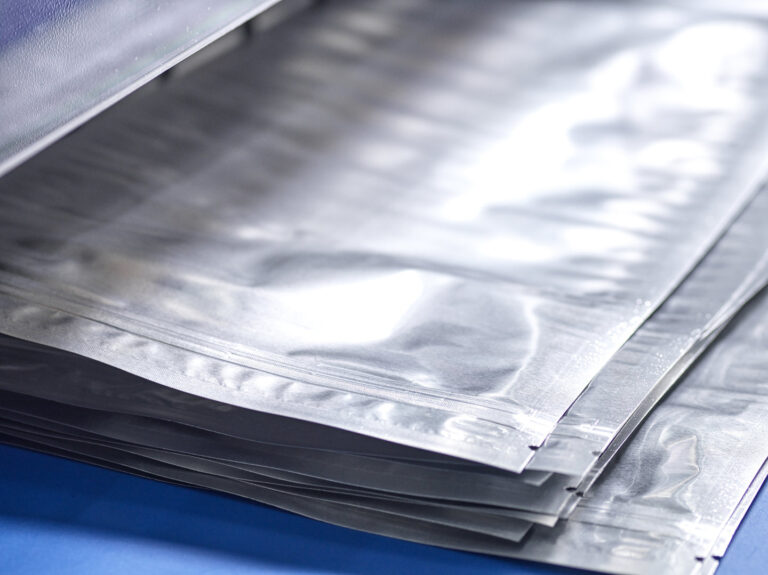
Tailored Solutions for Every Pharmaceutical Format
No two pharmaceutical operations are alike. That’s why we offer a versatile range of customisable barrier foil products designed for compatibility with your existing processes and packaging formats:
Gusseted Barrier Bags
Ideal for bulk packaging, our gusseted barrier bags are made to fit the inner dimensions of octabins, corrugated boxes or FIBCs. These liners accommodate large volumes while providing a physical and climatic shield—preserving product integrity from fill to delivery.
Custom Pouches
For smaller volumes, our flat barrier pouches offer a compact yet high-performance alternative. Manufactured to your exact size and laminate specification, these pouches are ideal for intermediate compounds, APIs, or specialty pharmaceuticals. No minimum order quantities and fast turnaround times make them a flexible, scalable option.
Form-Fill-Seal (FFS) Tubing & Sheeting
Our continuous rolls of single-wound aluminium foil sheeting are engineered for automated, high-speed production lines. Available in a variety of FDA-compliant laminate grades, FFS materials ensure consistent sealing, ease of use, and reliable protection in high-output operations.
Compliance, Confidence, and Customisation
All of our pharmaceutical packaging solutions are manufactured to meet international health and safety regulations, including FDA and EU directives. With ISO 9001:2015 accreditation, rigorous in-house quality control, and years of industry expertise, we are your trusted partner in delivering safe, compliant, and effective pharmaceutical packaging.
Let’s Protect Your Product, Together
When failure isn’t an option, our barrier foil packaging ensures that your pharmaceutical goods arrive exactly as intended—potent, pure, and protected.
Do you have a need you would like to discuss?
Talk to our team of experts who will be happy to work with you to develop a solution.